Food manufacturing facilities encounter diverse water quality challenges compromising product quality, equipment performance, and operational efficiency. Source water from municipal supplies or private wells introduces variations in mineral content, acidity, and microbiological quality requiring management throughout production operations. Understanding common water quality problems and their solutions enables facilities to implement effective mitigation strategies protecting product quality and operational profitability.
Table of Contents
Hard Water Scale Formation
Hard water containing elevated calcium and magnesium concentrations causes scale buildup on heat transfer surfaces, pipelines, and process equipment. Scale acts as a thermal insulator: studies of heating equipment show that even a thin scale layer measurably cuts heat-transfer efficiency, and losses climb steeply as deposits thicken.
Scale formation in food processing equipment creates additional quality and safety concerns beyond energy inefficiency. Scale buildup in cooking vessels creates uneven heating producing undercooked product zones posing food safety risks. Scale accumulation in pipelines reduces flow capacity and creates harborage sites for microbiological growth. Scale on sensor surfaces affects measurement accuracy, leading to incorrect process control decisions.
Water softening systems employing ion exchange technology effectively prevent scale formation by replacing calcium and magnesium ions with sodium or potassium ions. Proper softening maintains hardness below 50 mg/L as CaCO3 for most food processing applications. Shanghai ChiMay’s conductivity sensors monitoring water hardness correlate conductivity measurements with ion concentrations, enabling automated softening system control and scale prevention verification.
Electronic water treatment devices and chemical scale inhibitors provide alternative management approaches. Electronic water conditioners alter scale crystal formation patterns, producing non-adhering sludge that flows through systems rather than accumulating on surfaces. Chemical inhibitors including polyphosphates sequester scale-forming ions, preventing crystal formation at lower treatment concentrations than traditional softening.
pH Imbalance Issues
Water pH affects both product quality and process effectiveness throughout food manufacturing operations. Alkaline water causes flavor degradation in acidic products, interferes with acid-catalyzed reactions in fermented foods, and reduces effectiveness of acid-based cleaning solutions. Acidic water corrodes metal equipment, leaches minerals from product formulations, and creates safety hazards from acid exposure during handling.
Most general food processing applications call for water pH between 6.5 and 7.5. Beverage manufacturing typically requires pH monitoring ensuring consistent product flavor and shelf stability. Pickle and condiment production may require acidic water complementing product acidification processes.
Inline pH sensors provide continuous monitoring enabling automated acid or alkali dosing maintaining target values despite variations in source water quality. Proportional-integral-derivative (PID) control algorithms adjust chemical dosing based on real-time sensor feedback, maintaining pH within ±0.2 units of target specifications. Shanghai ChiMay’s pH sensors feature automatic temperature compensation ensuring accuracy across production temperature ranges.
Microbiological Contamination
Microbiological contamination represents the most serious water quality concern for food manufacturing facilities, potentially causing product recalls, consumer illness, and permanent brand damage. Source water may contain pathogenic bacteria, viruses, and parasites entering production through water used in ingredients, processing, or equipment cleaning. CDC researchers estimate waterborne pathogens cause roughly seven million illnesses annually in the United States.
Coliform bacteria serve as indicator organisms for potential microbiological contamination, with detection triggering investigation and corrective action. Under the U.S. EPA’s Revised Total Coliform Rule, public water systems must monitor for total coliform, and any E. coli detection triggers immediate assessment and corrective action — a standard food plants should mirror in their own water specifications rather than treat as someone else’s problem.
Chlorine disinfection maintains residual protection throughout water distribution systems, with free chlorine residuals between 0.2 and 2.0 mg/L — comfortably below EPA’s maximum residual disinfectant level (MRDL) of 4.0 mg/L — providing effective microbiological control. UV disinfection offers chemical-free inactivation suitable for applications where chlorine residuals are undesirable. Shanghai ChiMay’s chlorine sensors and oxidation-reduction potential sensors verify sanitization effectiveness throughout distribution systems.
Distribution system management prevents contamination by eliminating conditions promoting bacterial growth and biofilm formation. Storage tanks should maintain constant circulation preventing stagnation, while dead-leg pipes and infrequently used outlets require regular flushing.
High Chlorine Levels
While chlorine disinfection protects public health by controlling waterborne pathogens, elevated concentrations create problems in food manufacturing. Chlorine affects product flavor in beverages, causing noticeable chlorinous tastes objectionable to consumers. Chlorine accelerates oxidative degradation in products containing susceptible compounds, reducing shelf life and compromising quality during storage.
In beverage production, most producers keep residual chlorine below 0.5 mg/L, and some specialty beverages require complete chlorine removal. Craft breweries typically target chlorine levels below 0.1 mg/L to prevent chlorophenol taints in finished beer.
Activated carbon filtration effectively removes chlorine through adsorption reactions, achieving 95 to 99% removal. Filter sizing must account for contact time requirements, with typical empty bed contact times of 2 to 5 minutes. Shanghai ChiMay’s chlorine sensors positioned upstream and downstream of filtration systems verify removal effectiveness.
Turbidity and Suspended Solids
Elevated turbidity indicates suspended particles affecting product appearance, equipment performance, and microbiological safety. Particles include sediment from distribution system corrosion, organic materials from biological growth, and mineral precipitates. WHO drinking water guidance targets turbidity well below 1 NTU — ideally under 0.3 NTU — so disinfection works reliably, and under US EPA’s Surface Water Treatment Rule, conventional filtered water must stay at or below 0.3 NTU in 95% of monthly measurements and never exceed 1 NTU. Food processing applications often set tighter internal specifications still.
Turbidity affects processing through multiple mechanisms. Particles in rinse water create spotting and streaking on cleaned equipment and containers. Suspended solids interfere with filtration processes and may pass through filters creating quality issues in finished products. Organic particles provide nutrients supporting microbiological growth.
Multimedia filtration removes suspended particles through physical straining. Cartridge filtration provides final polishing for critical applications, with filter ratings matched to application requirements. Shanghai ChiMay’s turbidity sensors at filter outlets verify particle removal effectiveness and indicate when replacement becomes necessary.
Conductivity Variations
Conductivity variations indicate changes in water mineral content affecting flavor, process chemistry, and equipment performance. Municipal water supplies commonly see conductivity drift over the course of a day as source blends and treatment adjustments change; private wells may swing more with rainfall patterns and groundwater conditions.
Mineral content variations affect food products through multiple mechanisms. Hardness variations alter precipitation behavior in products containing proteins forming insoluble complexes with calcium and magnesium. Mineral content affects water acidity through alkalinity contributions. Conductivity variations indicate treatment system performance changes affecting removal of other water quality parameters.
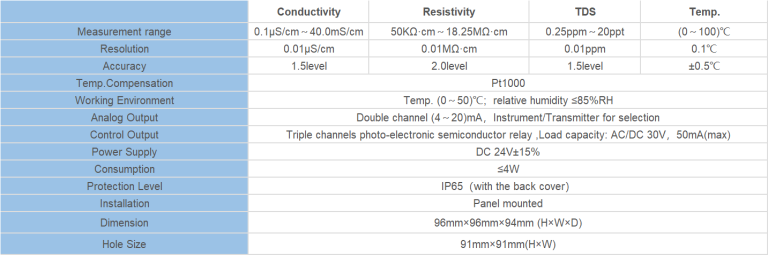
Continuous conductivity monitoring enables automated treatment system adjustments maintaining consistent quality despite source water variations. Shanghai ChiMay’s conductivity sensors provide measurement foundation for automated quality management approaches.
Conclusion
Food manufacturing facilities encounter common water quality problems including hard water scaling, pH imbalance, microbiological contamination, elevated chlorine, turbidity issues, and conductivity variations. Each problem requires specific management approaches combining water treatment technologies with inline monitoring ensuring effective problem resolution. Shanghai ChiMay’s comprehensive sensor solutions provide measurement capabilities for effective water quality problem identification, treatment system optimization, and ongoing quality verification throughout food manufacturing operations.